7 Best Ways to Ensure Quality in Steel Structure Projects?

Time:2026-10-08 Author:Mason
0%

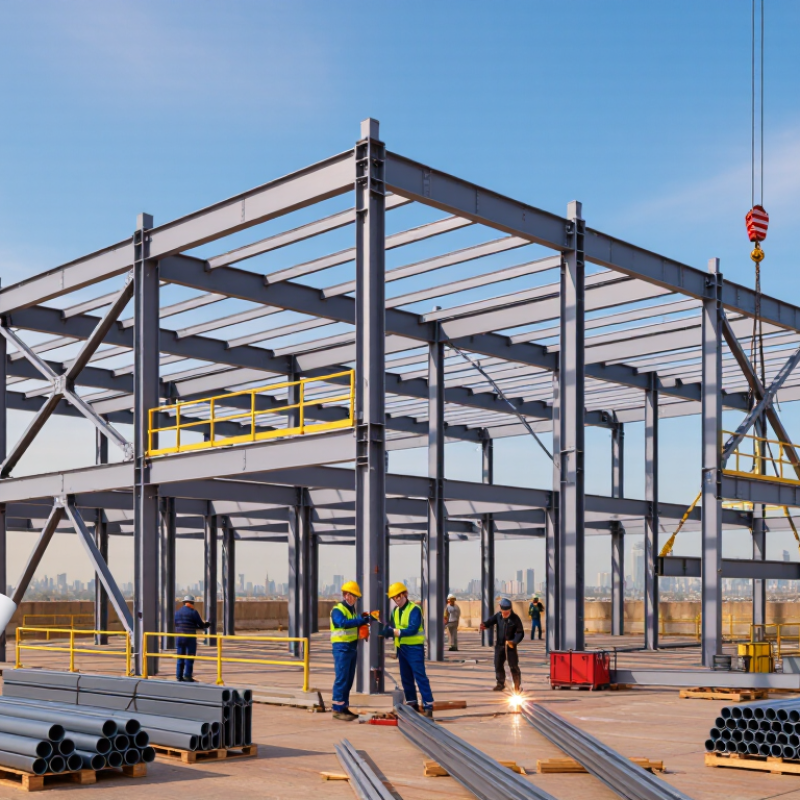
Steel structures rarely fail because of one dramatic mistake. More often, quality weakens through small gaps in design review, fabrication, transport, and site assembly. A slightly misplaced bolt hole can delay an entire connection. An unnoticed weld defect may remain hidden beneath protective coating. These details explain why how to ensure quality in steel structure projects requires more than a final inspection.

Reliable quality begins with practical control at every project stage. Experienced engineers verify drawings, load requirements, material grades, and connection details before fabrication starts. Certified suppliers should provide mill certificates and traceable batch information. In the workshop, inspectors can check cutting accuracy, weld preparation, welding parameters, and dimensional tolerances. Clear records matter. They help teams identify problems before steel reaches the site.

Site conditions add another layer of risk. Rain, poor storage, rushed lifting, and missing temporary bracing can damage otherwise compliant work. Independent inspections, non-destructive testing, coating checks, and properly calibrated tools provide stronger evidence than assumptions. However, no quality system is perfect. Teams may overlook a recurring issue when production pressure rises. That weakness deserves honest review, not concealment. Regular toolbox meetings, documented corrective actions, and communication between designers, fabricators, inspectors, and installers create accountability. The following seven approaches explore practical ways to protect structural performance, worker safety, project schedules, and long-term durability. Good quality is not merely paperwork. It is steel that fits, performs, and remains dependable years after handover.
7 Best Ways to Ensure Quality in Steel Structure Projects?

Set Quality Criteria with ISO 9001, AISC 360, and EN 1090-2

Quality begins before steel reaches the workshop. Define measurable criteria in a project quality plan. Use ISO 9001 to control documents, responsibilities, audits, and corrective actions. Map each requirement to a drawing, inspection point, or test record. Use AISC 360 for structural design and execution expectations. Apply EN 1090-2 when fabrication, welding, and execution classes require European controls. Standards guide decisions, but they do not replace engineering judgment.

Quality Control Check seven practical areas: qualified personnel, approved drawings, traceable steel certificates, controlled cutting, qualified welding procedures, dimensional inspections, and protected delivery. Keep heat numbers linked to members. Photograph bolt installation and weld preparation. Measure column plumbness with calibrated instruments. Record coating thickness after surface preparation. Small details matter. A missing calibration record can weaken an otherwise sound inspection file.

Independent hold points can stop defects before erection. Inspectors should verify fit-up before welding and bolts before final tightening. Nonconformance reports need causes, owners, deadlines, and evidence of closure. Site teams should compare actual conditions with approved drawings daily. In practice, rushed revisions still create confusion. That weakness deserves review. Quality improves when lessons return to the plan, not when paperwork merely grows.

Verify Steel Materials Using EN 10204 Type 3.1 Certificates

7 Best Ways to Ensure Quality in Steel Structure Projects?

Verify Steel Materials Using EN 10204 Type 3.1 Certificates

An EN 10204 Type 3.1 certificate links delivered steel to its tested production batch. It normally includes the material grade, heat number, dimensions, chemical composition, and mechanical test results. The manufacturer’s authorized inspection representative validates these results independently from the production process.

At delivery, compare the certificate with the purchase specification and packing list. Check every heat number stamped on plates, beams, or hollow sections. Confirm that yield strength, tensile strength, elongation, and impact values meet the required standard. Do not rely on a certificate that only lists general product properties. It should identify the actual supplied material.

Traceability is everything. Record the heat number during receiving inspection, then connect it to cutting lists, weld maps, and fabrication records. Paper alone is insufficient. Missing markings can create serious uncertainty later, especially after blasting or cutting. Some teams accept unclear documents to avoid project delays. That shortcut is tempting, but it weakens quality control. A certificate may also contain typing errors, so unusual values deserve clarification before fabrication begins. Keeping scanned certificates with inspection photographs makes future reviews faster and more defensible.

Control Welding Through AWS D1.1 WPS/PQR and Welder Qualification

7 Best Ways to Ensure Quality in Steel Structure Projects?

Control Welding Through AWS D1.1 WPS/PQR and Welder Qualification

Welding quality begins before the arc starts. A project team should prepare a clear Welding Procedure Specification based on AWS D1.1 requirements. The WPS defines joint details, base metals, filler materials, preheat, heat input, and welding positions. These details reduce guesswork on the fabrication floor. They also help inspectors compare actual work with approved limits. Small errors matter. A missing preheat record can weaken confidence in an otherwise acceptable weld.

The Procedure Qualification Record proves that the proposed method can produce sound welds. Test coupons should represent the real joint, thickness, process, and position whenever possible. Mechanical testing and visual examination provide useful evidence, not paperwork alone. Welder qualification is equally important. Each welder should perform a qualified test and work only within the approved range. Keep identification marks, continuity records, and inspection results traceable to each weld.

Experienced supervisors still need to watch the work closely. They check fit-up, root openings, surface cleanliness, electrode storage, and interpass temperature. Photos of tack welds and temperature readings can reveal repeated problems early. Non-destructive testing may support visual inspection, especially on critical connections. However, testing cannot repair poor preparation. Our field teams have learned that rushed production often creates more rework than it saves. Some procedures also look correct on paper but fail in crowded site conditions. Regular review is necessary, and admitting that weakness early protects both safety and schedule.

7 Best Ways to Ensure Quality in Steel Structure Projects

Control welding through AWS D1.1 WPS/PQR requirements and qualified welders.

The chart presents recommended 100% control-coverage targets for the seven core welding quality practices. Project teams should verify the applicable AWS D1.1 requirements, approved WPS or PQR documentation, welder qualification status, consumable control, fit-up and preheat conditions, inspection records, and non-destructive testing requirements before acceptance.

Inspect Bolted Connections with AISC Pretension Requirements

AISC-based steelwork depends on more than tightening bolts until they feel secure. Snug-tight is not the same as required pretension. The RCSC Specification for Structural Joints Using High-Strength Bolts, 2020, lists 28 kips for a 3/4-inch ASTM F3125 Grade A325 bolt. That force is substantial. It also varies with bolt diameter, grade, and connection design. Do not guess.

On site, inspectors should confirm bolt type, diameter, installation method, and washer placement before testing. Marking each completed connection helps prevent skipped bolts. Calibrated wrench testing, turn-of-nut verification, tension-control methods, or direct-tension indicators must follow the approved procedure. The RCSC specification requires verification testing before installation begins, not after defects appear. AISC 360-22 Chapter N also assigns inspection duties for pretensioned and slip-critical joints.

Small details matter. Threads should extend beyond the nut, while faying surfaces remain clean and properly prepared. Paint, mill scale, or dirt can change friction and reduce slip resistance. Check the lot identification and calibration records.

Keep photographs and test results with the inspection log. A missed washer is easy to overlook. I have seen good crews rush the final row, especially during cold-weather erection. That is where assumptions become expensive. Review the sequence again. Field conditions are rarely perfect.

Reference sources: RCSC 2020 Specification, Table 5.1; AISC 360-22, Chapter N.

Close Seven Quality Gates Through NCR Tracking and ISO 9001 Records

7 Best Ways to Ensure Quality in Steel Structure Projects?

Close Seven Quality Gates Through NCR Tracking and ISO 9001 Records

Steel structure quality improves when each stage has a visible control point. In my project reviews, seven gates work well: design, materials, fabrication, welding, surface preparation, erection, and final inspection. Each gate needs approved drawings, inspection criteria, and named responsibilities. Material certificates should match heat numbers and delivery records. Welders need valid qualifications, while weld maps identify every critical joint. These details prevent small errors from becoming expensive site repairs.

Nonconformance reports, or NCRs, connect problems with corrective action. Record the location, photograph, affected component, and inspection reference. Then identify the cause, not only the visible defect. An ISO 9001 record should show containment, responsibility, approval, and closure evidence. Repeated NCRs may reveal weak training or unclear drawings. That is uncomfortable, but useful. A closed form without verified correction is not quality control.

Tips:

  • Review NCR trends weekly.
  • Keep records beside the work.
  • Use simple checklists.
  • Do not sign incomplete inspections.
  • Confirm bolt torque with calibrated tools, and retain the readings.
  • Check coating thickness at several steel surfaces, especially edges and repaired areas.
  • Independent inspections can challenge familiar assumptions.
  • Still, paperwork can become excessive.
  • Teams should remove duplicate records without weakening traceability.
  • Quality gates must support decisions, not merely fill folders.

FAQS

Is snug-tightening enough for a pretensioned structural connection?

No. Snug-tight means the connected surfaces are drawn together. It does not prove the required bolt tension. A 3/4-inch high-strength bolt may require about 28 kips, depending on the specification and connection design.

What should an inspector check before testing bolts?

Confirm the bolt type, diameter, installation method, and washer placement. Check that threads extend beyond the nut. Mark each completed bolt. Small marks prevent skipped locations.

Which methods can verify bolt pretension?

Approved procedures may use calibrated wrench testing, turn-of-nut verification, tension-control methods, or direct-tension indicators. Verification testing should occur before installation begins. Testing after failures is too late.

Why do faying surfaces require close inspection?

Paint, dirt, and mill scale can change friction between steel surfaces. Reduced friction may lower slip resistance. Look closely around connection edges and cleaned areas. Clean surfaces matter.

What records should support bolt inspection?

Keep lot identification, calibration records, photographs, and test results. Store them with the inspection log. A missing washer can disappear inside a busy folder. Review the evidence, not just the signature.

How can quality gates improve steel structure projects?

Use control points for design, materials, fabrication, welding, surface preparation, erection, and final inspection. Each gate needs approved drawings, clear criteria, and assigned responsibility. Keep checklists near the work.

What information belongs in a nonconformance report?

Record the location, photograph, affected component, inspection reference, cause, containment, responsible person, approval, and closure evidence. Correcting the visible defect may not fix the real cause. Repeated reports can expose weak training or unclear drawings.

How should teams manage inspection paperwork?

Review nonconformance trends weekly and remove duplicate records without losing traceability. Do not sign incomplete inspections. Independent review can challenge familiar assumptions. Paperwork helps only when it supports decisions.

Conclusion

Ensuring quality in steel structure projects requires a systematic process covering design, materials, fabrication, assembly, and documentation. The key to understanding how to ensure quality in steel structure projects is to establish clear acceptance criteria based on ISO 9001, AISC 360, and EN 1090-2. Steel materials should be verified through EN 10204 Type 3.1 certificates, confirming grade, chemical composition, mechanical properties, and traceability before fabrication begins.

Welding quality depends on approved AWS D1.1 welding procedures, qualified welders, and properly maintained inspection records. Bolted connections should be checked according to applicable pretension requirements, including bolt condition, installation method, and achieved tension. Finally, seven quality gates can help control each project stage, from material receipt and fabrication to final inspection. Nonconformance reports should be tracked to closure, while inspection results, approvals, corrective actions, and ISO 9001 records provide reliable evidence that the completed structure meets specified safety, performance, and durability requirements.
Mason

Mason

Mason is a seasoned marketing professional with a deep expertise in the company's offerings and a passion for driving brand awareness. With a strong background in digital marketing strategies, he has an innate ability to connect with diverse audiences and effectively communicate product benefits.......